






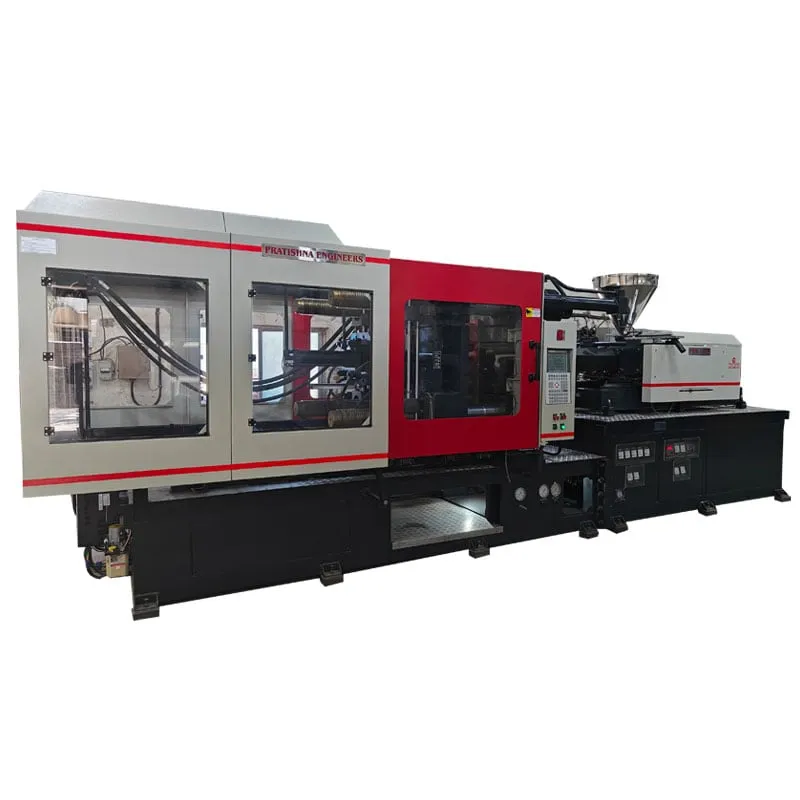

A plant head in Bhiwandi has quotations for three machines of the same tonnage, and they look nothing alike. One has a toggle clamp, one a hydraulic clamp and one a two-platen clamp; two run servo pumps and one is all-electric. Sorting the types of injection moulding machines into three questions makes that list readable: how the mould is clamped, what drives the motions, and whether the mould opens horizontally or vertically. Each answer changes the floor space, energy bill and parts you can run. Pick the clamp from the mould, the drive from your power bill, and the orientation from the part.
Key Takeaways
- Clamp type decides mould protection, opening stroke and machine length: toggle, direct hydraulic and two-platen each suit a different range of mould sizes.
- Drive type decides energy at idle: fixed-pump hydraulics cost the most to keep running, while servo, hybrid and all-electric drives cut the base load.
- Orientation decides handling: horizontal machines drop parts by gravity onto a conveyor, while vertical machines hold inserts still in an open lower mould half.
- Ten-year energy cost exceeds purchase cost in almost every case, so judge a drive type on running cost before you judge it on purchase cost.
What are the main types of injection moulding machines by clamp?
There are three main clamp types. A toggle clamp uses linkages to multiply a cylinder's force, a direct hydraulic clamp pushes the platen with oil pressure, and a two-platen clamp locks the moving platen with split nuts and then applies tonnage with short-stroke cylinders.
Toggles are defended for reliability, simplicity and rigidity, and suppliers report that they lock up slightly faster and give greater opening force, which suits deep-draw parts. Their limits are a narrower stroke-adjustment range and a risk of over-clamping if die height is set with the mould closed and it then warms and expands. Toggle linkages also need lubrication, and grease can reach the mould area if seals and wipers are neglected.
Direct hydraulic clamps are reported to give finer pressure control, more uniform pressure on the mould and better mould protection, with a wider die-height range. Two-platen clamps shorten the machine, which matters most on large tonnages where a toggle frame for the same mould would be long.
Stroke behaves differently on each. A toggle gives its full stroke at every shut height, while a piston or two-platen clamp loses stroke as the mould gets taller and reaches maximum stroke only at minimum shut height. For tall parts, compare daylight minus mould height, never the headline stroke figure.
Clamp types compared
| Clamp type | How it applies tonnage | Reported strengths | Watch for |
|---|---|---|---|
| Toggle | Linkages multiply a cylinder's force | Simple, rigid, fast lock-up, high opening force | Stroke adjustment, over-clamp on a warm mould, linkage wear |
| Direct hydraulic | Large cylinder pushes the platen | Fine pressure control, mould protection, wide die-height range | Oil volume and pump energy |
| Two-platen | Split nuts lock, short-stroke cylinders clamp | Shorter machine, suits large moulds | Stroke falls as mould height rises |
Hydraulic, servo, hybrid or electric: which drive suits you?
The drive decides how much power the machine draws when it is not moving much. Fixed-pump hydraulics draw heavily even at idle, servo-pump hydraulics slow the motor when oil is not needed, hybrids add electric axes, and all-electrics drive every motion with servo motors.
Base load tells most of the story. On a standard hydraulic machine it can be 75% or more of total energy, and a high base load can mean the machine is too large for the job. On all-electric and hybrid machines it is about 10 to 20%, mostly barrel heating. Measure before you buy: a clamp-meter data logger can profile a machine in as little as 30 minutes.
Many older machines with fixed-speed pumps are still in service, with very high energy demand. Retrofit options include variable-speed motors, variable-volume pumps and servo motors on fixed pumps. An electric screw drive can also cut peak power and let you downsize the main motor. Rising energy on the same job can also point to screw or barrel wear, so log it before and after any change.
In Maharashtra, the drive also shows up on your bill. MSEDCL bills HT consumers and LT consumers above 20 kW in kVAh, so a poor power factor costs you directly: at 0.85, every 100 kWh is billed as about 117.6 kVAh. Ask what power factor each drive runs at, and plan APFC panels where needed.
Drive types and base load
| Drive | How motions are driven | Base load | Fits |
|---|---|---|---|
| Fixed-pump hydraulic | Constant-speed motor and pump | Can be 75% or more of total energy | Older machines, retrofit candidates |
| Servo-pump hydraulic | Motor slows when oil is not needed | Lower; some new hydraulics come close to all-electric use | General moulding with high clamp forces |
| Hybrid | Hydraulic clamp with electric axes such as screw or injection | About 10 to 20%, mostly barrel heating | Large clamps with lower idle energy |
| All-electric | Servo motors on every axis | About 10 to 20%, mostly barrel heating | Jobs that idle often, repeatable shots |
Horizontal or vertical: how does orientation change the job?
Horizontal machines open sideways, so moulded parts fall by gravity onto a conveyor or are picked by a robot, which suits most high-volume parts. Vertical machines open upwards, so inserts placed in the lower half stay where they are put, which suits insert and overmoulding work.
Horizontal is the default for a reason: unattended running is easier when parts drop clear and the next shot can start at once. Mould change, cooling water connections and robot mounting are all straightforward on a horizontal frame. Robots, conveyors and stack moulds all assume parts can leave the mould sideways and fall clear.
Vertical machines trade that for stable insert loading and a small footprint, and they often carry shuttle or rotary tables so one lower half is loaded while the other moulds. Treat them as a deliberate choice for insert parts, not a general alternative to a horizontal press.
Orientation sits alongside clamp and drive rather than replacing them. Describe each machine by all three answers, clamp, drive and orientation, when you compare quotations, and ask each supplier to state them on the same sheet so that you compare like with like.
What should you decide first when comparing machine types?
Decide in this order: the part and mould first, then orientation, then clamp, then drive. Send your part drawing, mould size and height, resin and monthly volume, and ask each supplier to state all three answers for the machine they propose. Ask for a trial on your own mould before you commit. See the full injection moulding machine range.
Frequently Asked Questions About Types of Injection Moulding Machines
Is a toggle or a hydraulic clamp better for precision parts?
Neither wins outright. Toggles are valued for rigidity and fast lock-up, while direct hydraulic clamps are reported to give finer pressure control and more uniform pressure on the mould. Precision depends more on platen parallelism, injection control and mould quality, so judge the whole machine on a trial with your own mould.
What is a hybrid injection moulding machine?
A hybrid mixes hydraulic and electric drives on one machine, such as a hydraulic clamp with electric injection or screw rotation. Most newer hybrid clamps are two-platen designs with hydromechanical locking. The aim is a lower base load than a full hydraulic machine, while keeping hydraulic force where it helps, such as high-tonnage clamping.
Can an old hydraulic machine be converted to a servo drive?
Often, yes. Retrofit options include variable-speed motors, variable-volume pumps and servo motors driving fixed pumps. Start by listing each machine's motor and pump type, measure its energy on a typical job with a clamp-meter data logger, and compare the result with what a servo retrofit would save before you decide.
Why does a two-platen machine take less floor space?
A two-platen clamp has no toggle linkage or long clamp cylinder behind the moving platen. It locks the platen with split nuts and builds tonnage with short-stroke cylinders, so the clamp end is shorter. The saving matters most on large tonnages, where a toggle frame for the same mould would be long.
Should a small unit buy an all-electric machine?
Only if the numbers support it. All-electric machines cut base load and give repeatable shots, and they pay best where machines idle often or run demanding parts. Measure what your current machines draw on typical jobs, check your kVAh bill and power factor, and compare running cost over several years, not purchase cost alone.
Related Articles
- Vertical Injection Moulding Machine
- Hybrid Injection Moulding Machine: Revolutionizing Production
- The Role of Toggle Moulding Machines in High-Precision Manufacturing
- Best Injection Moulding Machines for Plastic Industry in India
Sources & References
- Plastics Technology, M. Knights: Hybrid Injection Clamps: The Best of Both Worlds?
- ExxonMobil, AMI and Tangram Technology: An Energy Saving Guide for Injection Moulders
- SPE Plastics Engineering, R. Kent (Tangram Technology): Energy-Saving Tip 67: Injection Molding: get the right motor
- MSEDCL: kVAh Billing: Frequently Asked Questions
Technical Disclaimer
Disclaimer: The information provided in this document is for general informational and educational purposes only. It is based on technical references and industry information available at the time of preparation and may be subject to change. It does not constitute engineering, technical, commercial or professional advice, nor does it constitute a quotation, specification, warranty or contractual commitment by Pratishna Engineers.
Actual injection moulding machine and process requirements vary according to the component design, material, mould, production volume, machine configuration and operating conditions. The information, examples, calculations and recommendations provided should be independently evaluated and verified for the specific application before making any equipment, process or production decision. Information obtained from third-party sources remains subject to the accuracy and limitations of those sources.
Limitation of Liability: Pratishna Engineers makes no representation or warranty, express or implied, regarding the completeness, accuracy or suitability of the information for any particular application. To the extent permitted by applicable law, Pratishna Engineers shall not be liable for any loss, damage, cost or consequence arising from reliance on or use of the information contained in this document. Final machine selection, configuration and application suitability should be confirmed with Pratishna Engineers based on complete and accurate project requirements.

