Injection Moulding Machine for Connector Backshells, Inserts and Cable Glands
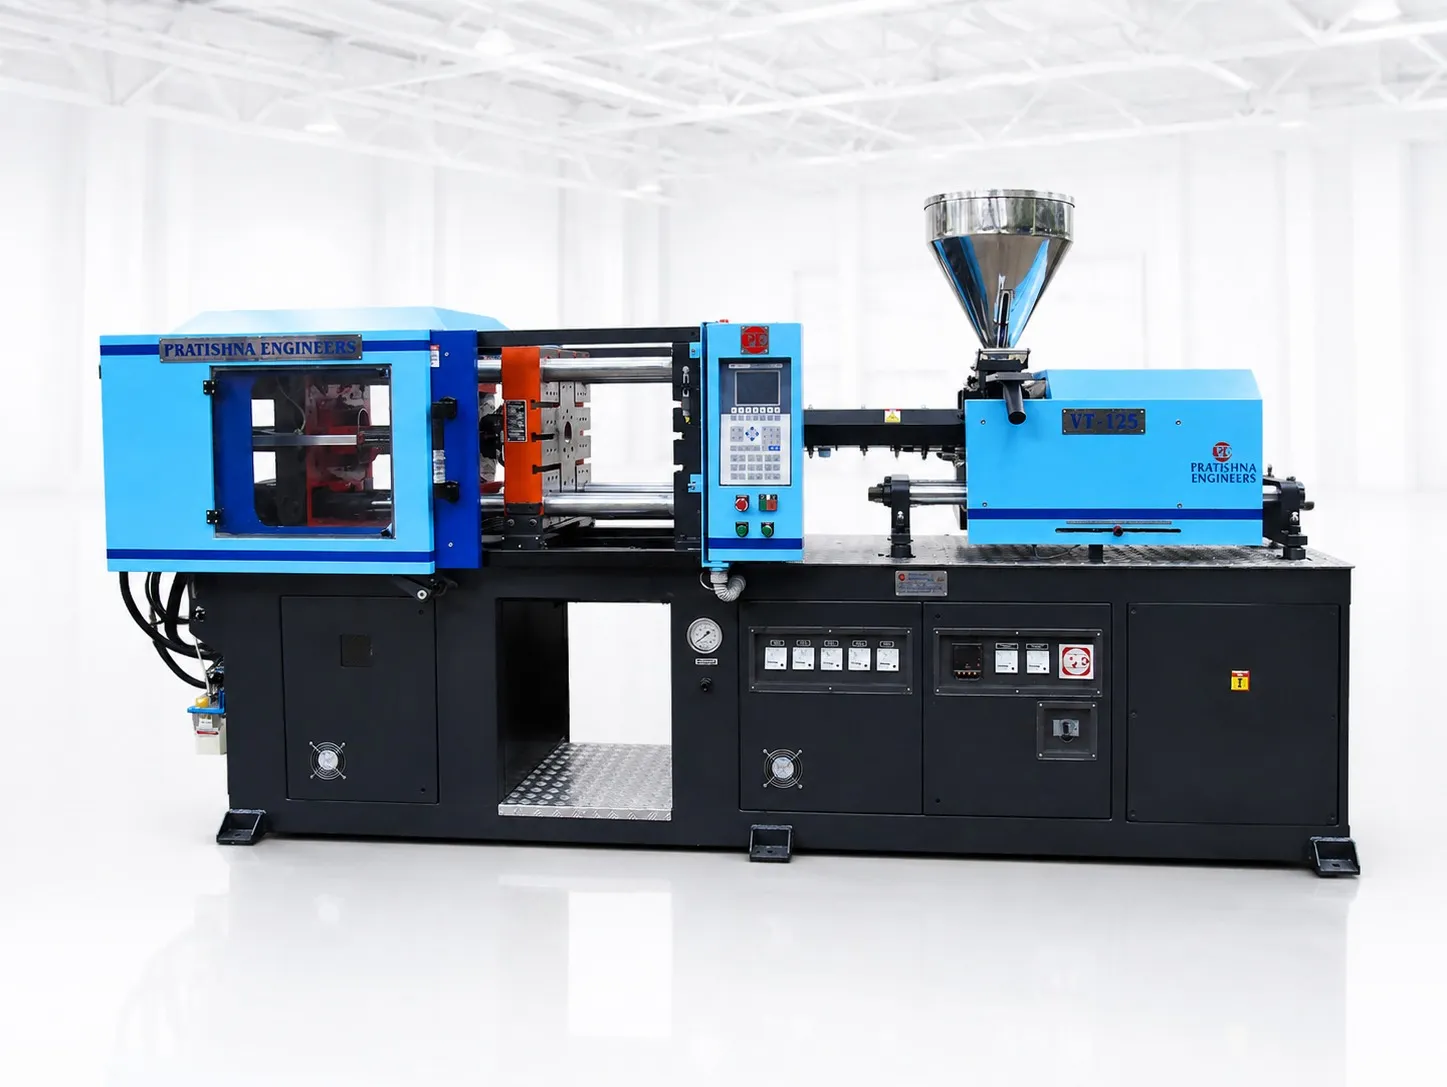
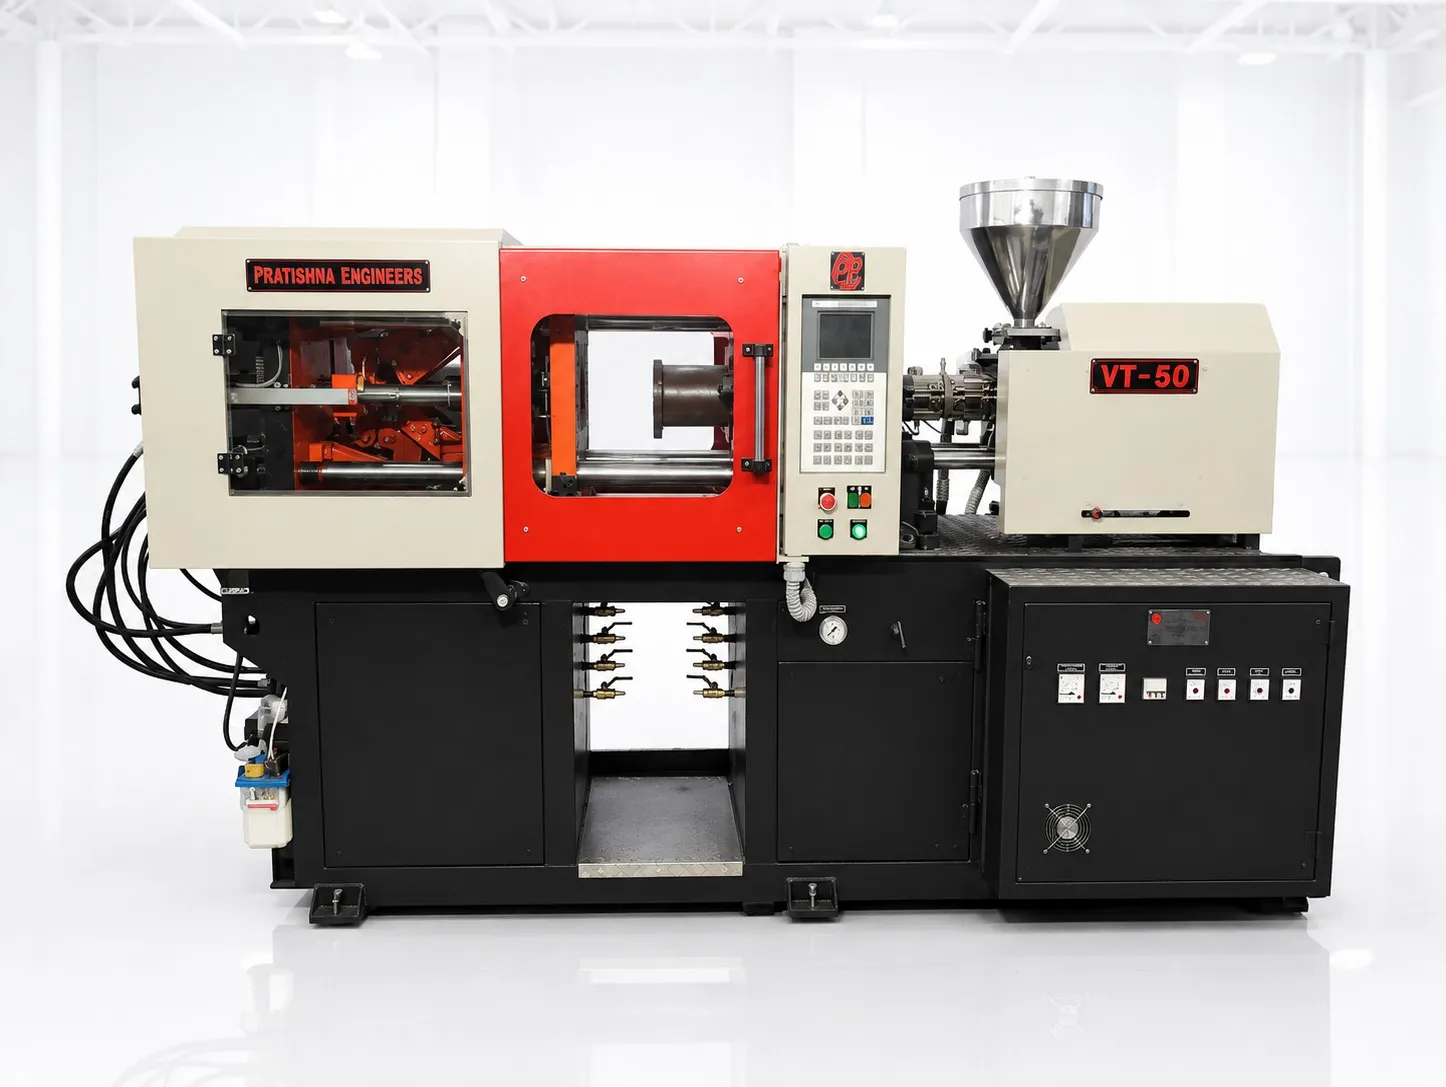
Connector backshells, contact inserts and cable glands are made on vertical insert-moulding injection moulding machines, or horizontal machines for parts without inserts, from glass-filled PA66 or PBT, PPS and PEI. Insert loading and cavity count set the machine. Flash control matters most, since flash in a contact bore scraps the part.
For these parts, machine selection weighs insert handling, accurate control of small shots and barrel heat for high-temperature grades. Pratishna Engineers supplies vertical and horizontal injection moulding machines for connector parts and can recommend a configuration for your insert and mould.
Moulding Connector Backshells?
Share your part drawing, insert details and material grade, and Pratishna Engineers will recommend a vertical or horizontal machine.
Machine Requirements for Connector Backshell Moulding
Connector parts are small, insert-loaded and dimension-critical, so the machine must suit these points:
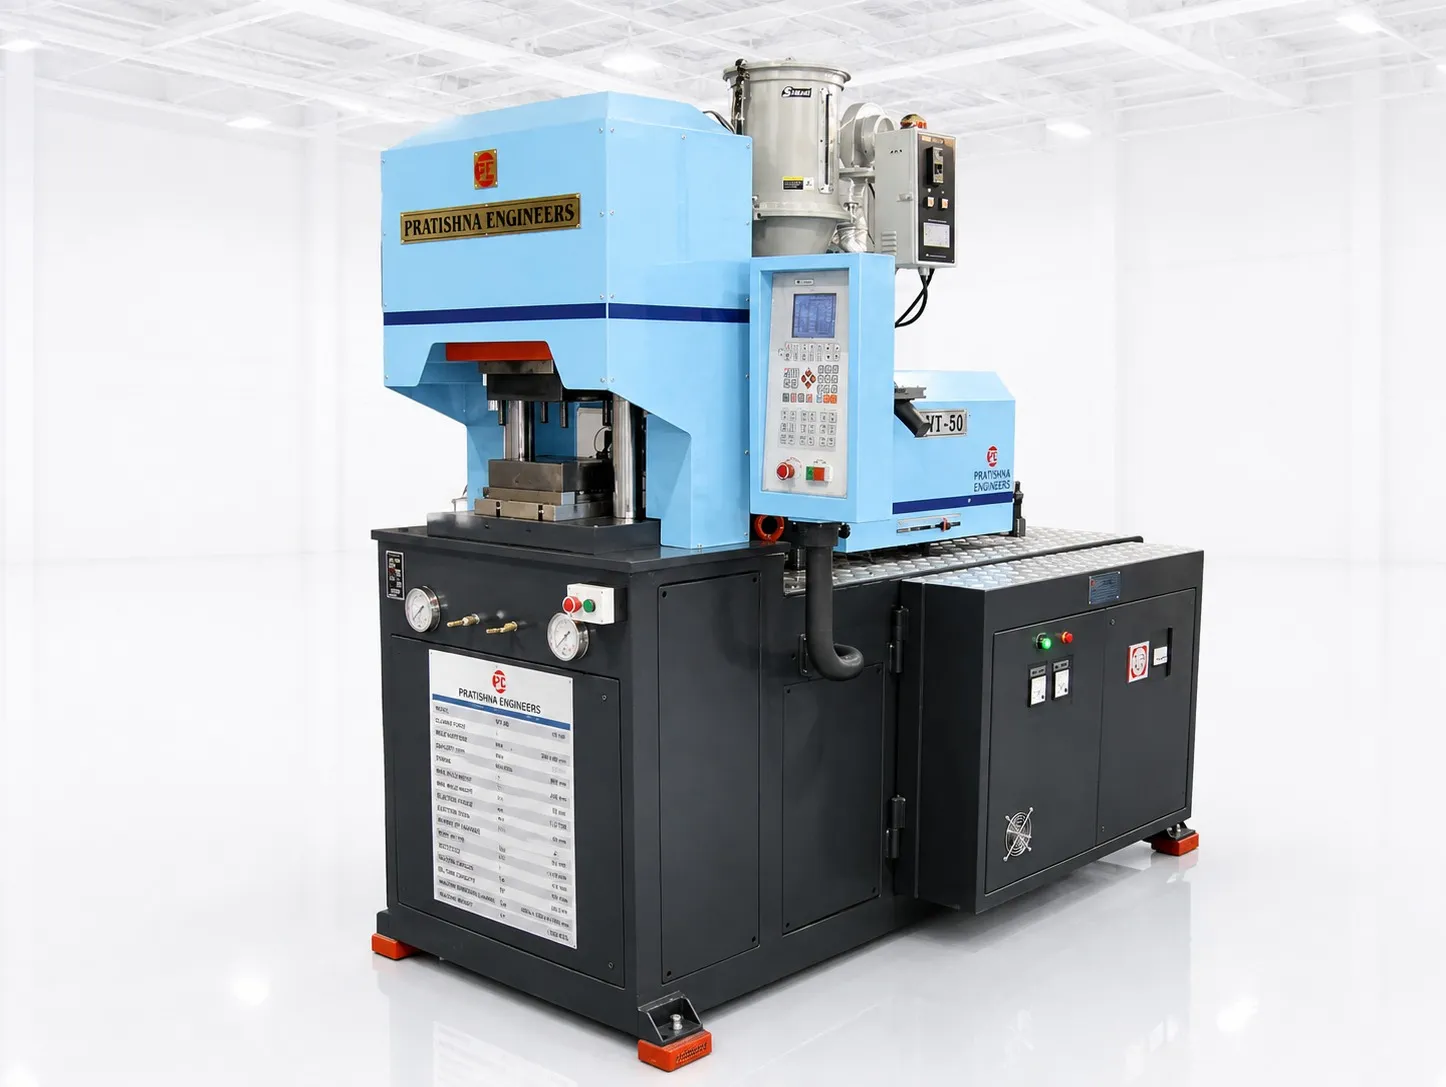
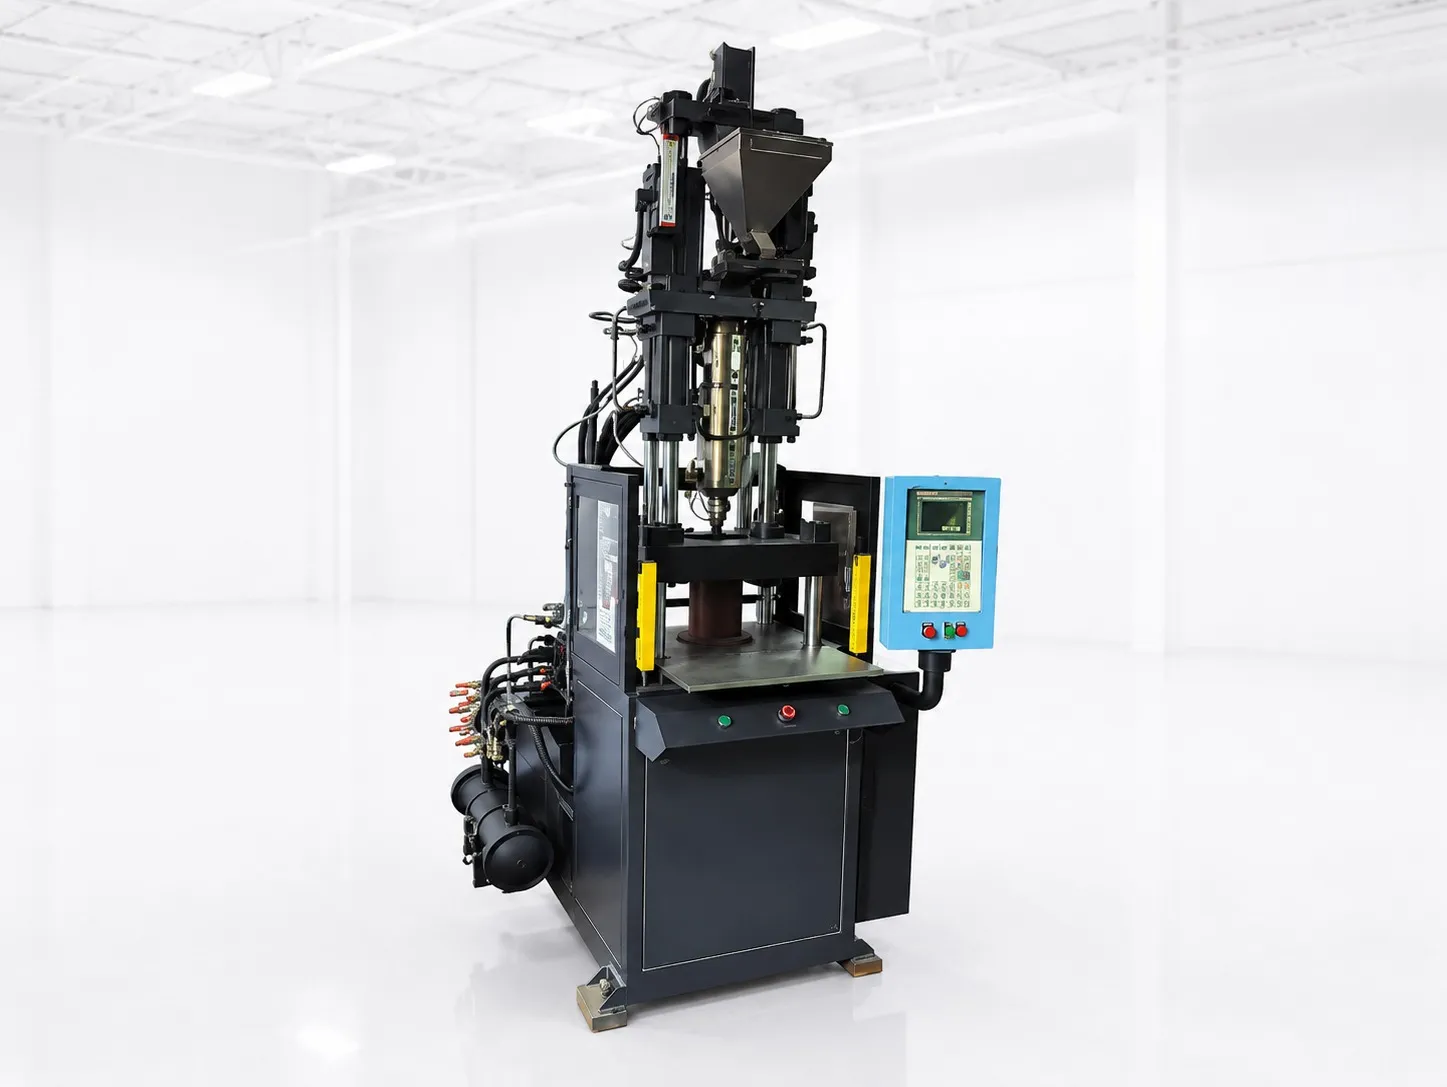
- Vertical clamp so metal inserts stay located by gravity
- Shut-off faces that keep flash out of contact bores
- Contact spacing held through steady shrinkage
- Barrel and nozzle heat for PPS and PEI
- Drying of PA66, PBT and PEI before moulding
- Insert preheating to cut stress around threaded shells
Recommended Machine for Connector Backshells
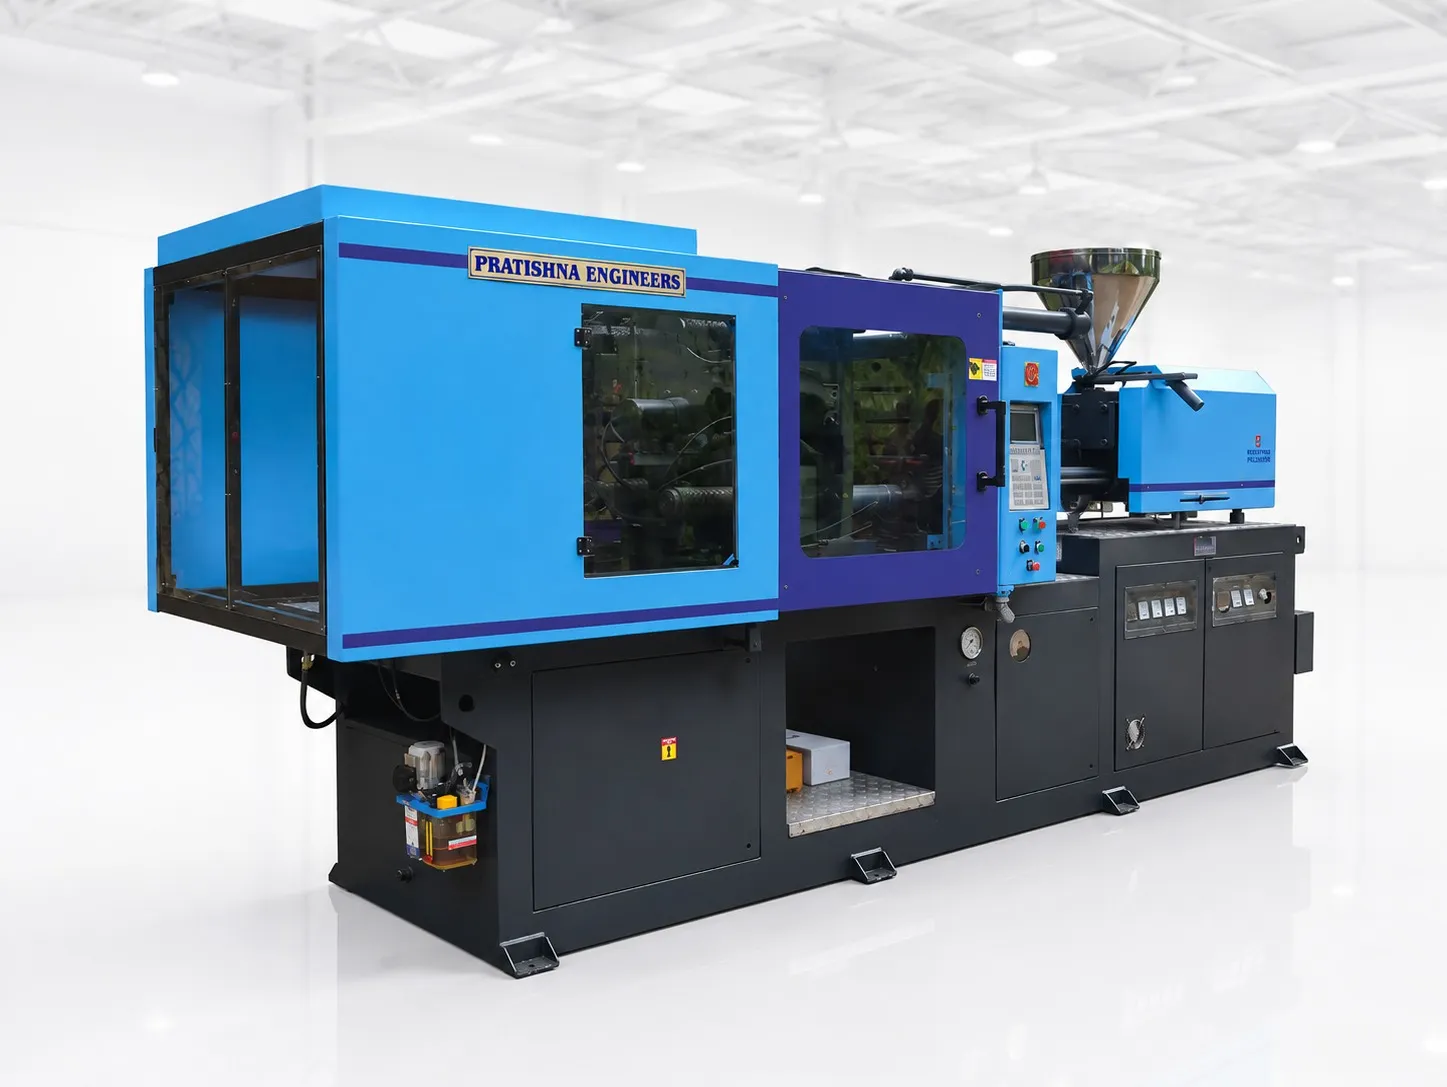
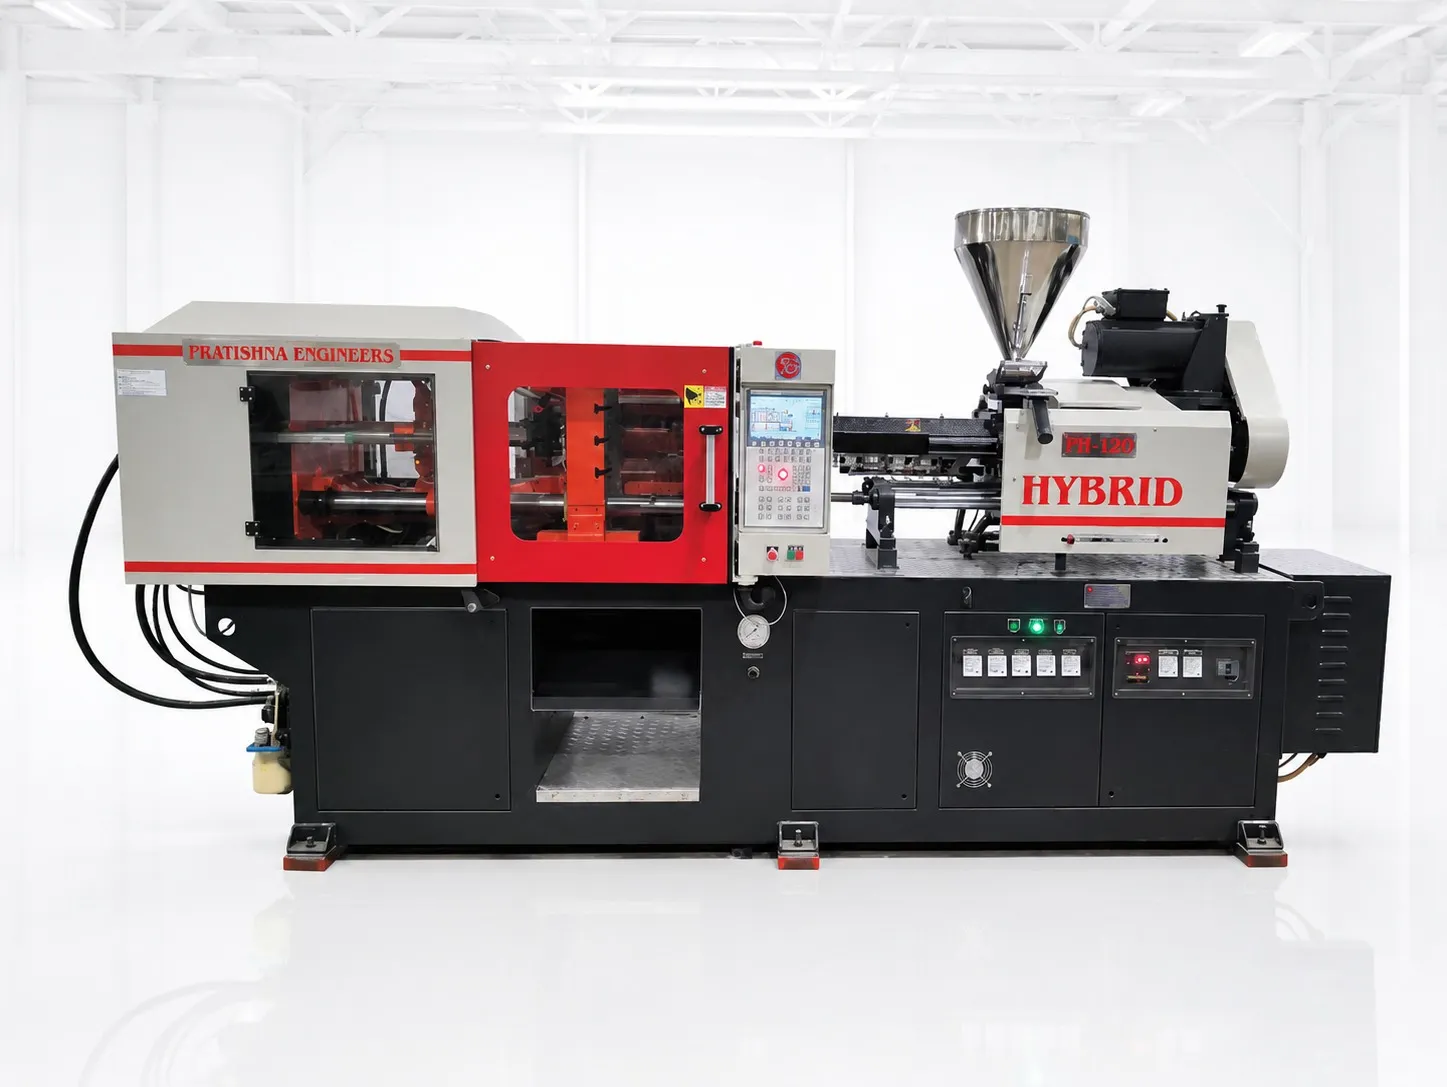
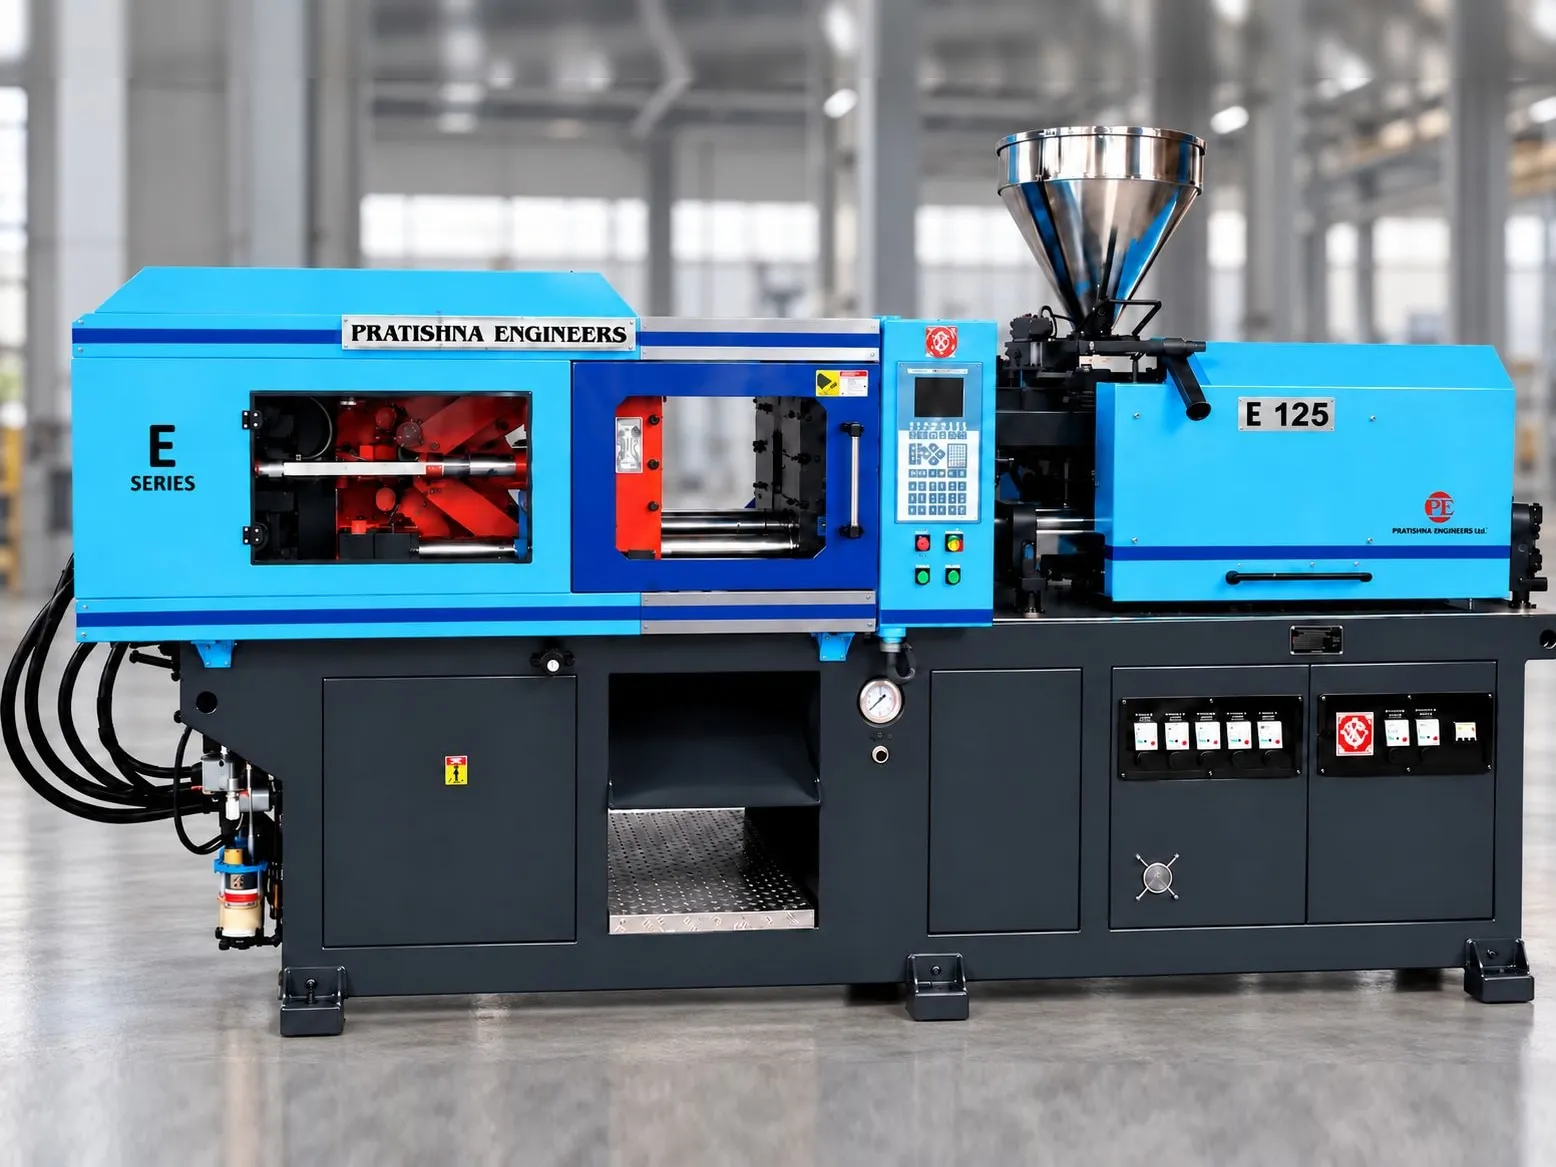
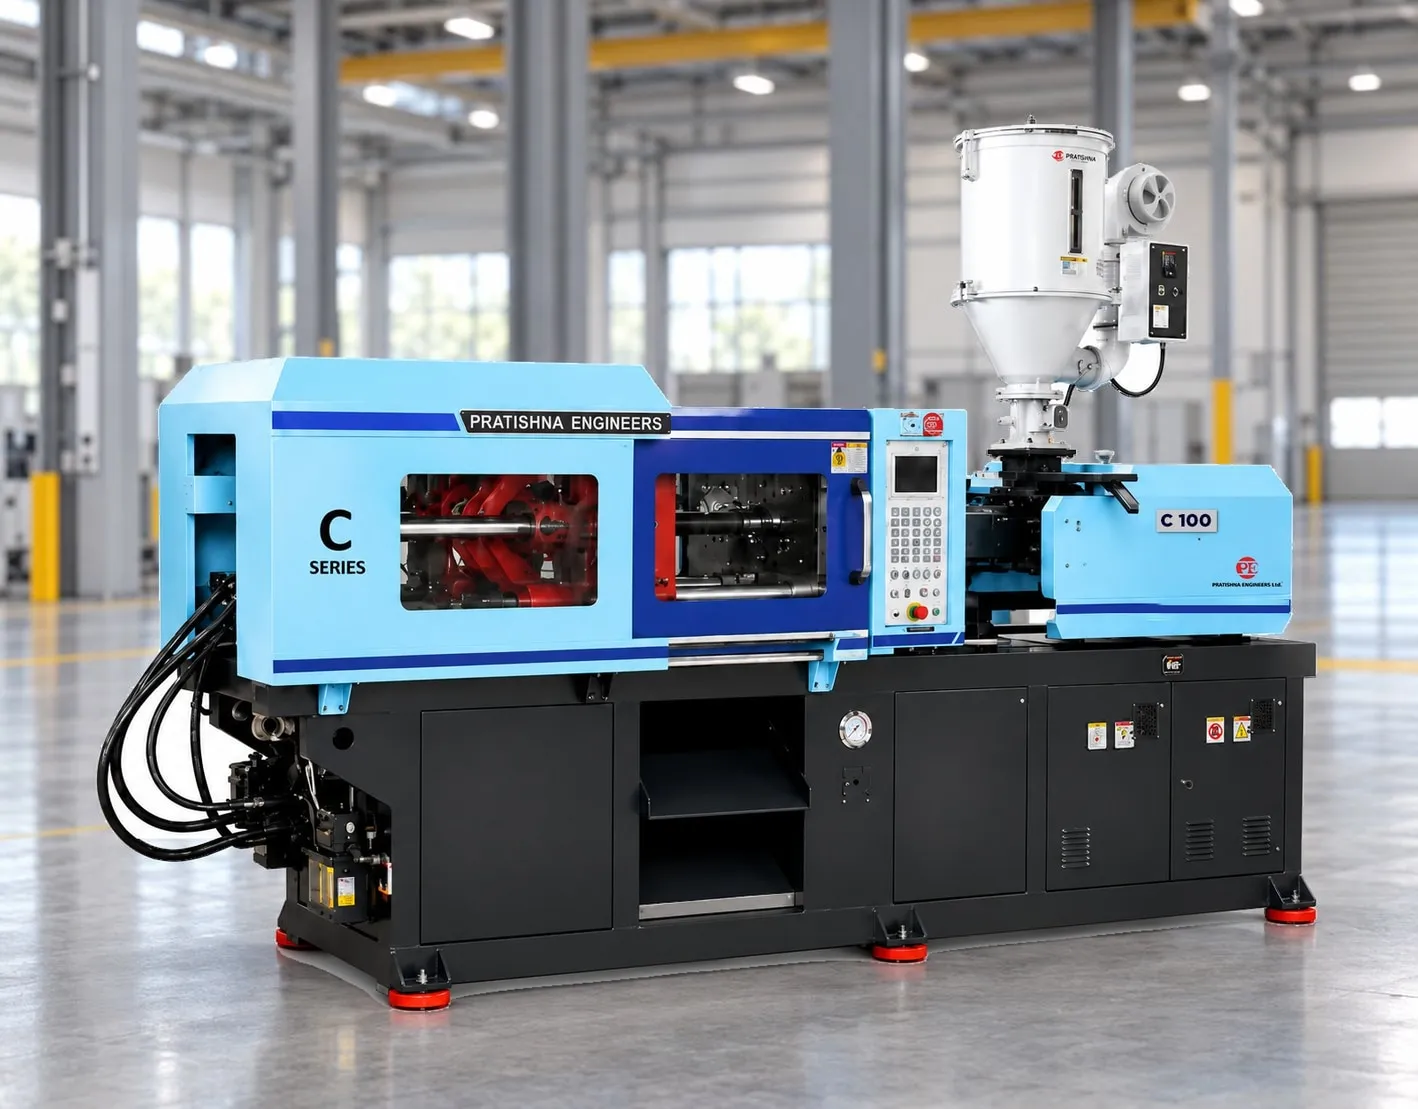
Insert-moulded backshells and contact inserts suit the vertical PVDL Series (40-80 T), where metal contacts and threaded shells are placed in the lower mould half. Parts moulded without inserts, such as gland nuts and plain backshell covers, run on the E Series (75-180 T), with the C Series (140-320 T) for multi-cavity moulds at the top of the size range.
Not Sure Which Machine You Need?
Share your insert and connector drawings for a machine recommendation.
Why Choose Pratishna Engineers?
- Application-Based Machine Selection
- In-House Engineering & Manufacturing
- Multiple Machine Series
- Production-Focused Solutions
- End-to-End Technical Support
- Industry-Specific Solutions
- Machine Lifecycle Support
Injection Moulding Machine Buyer Resources
Download practical resources to help you select, size and specify the right machine.
Vertical Injection Moulding Machine Selection Guide
A step-by-step guide covering the key inputs needed to select the right machine: product weight, insert type and loading method, projected area, number of cavities, plastic material, required clamping force, shot / injection capacity, mould dimensions, production quantity, cycle time and automation requirement.
Download PDFPDF · 265 KB
How to Calculate Clamping Force for an Injection Moulding Machine
A clear methodology that explains how clamping force is calculated, covering projected area, injection pressure, safety factor, number of cavities and material considerations.
Download PDFPDF · 363 KBDefence Sector Components & Machine Guide
A guide to Defence Sector components, covering drone frames, propellers, cowlings, gimbal housings, rugged enclosures, connector backshells and field battery housings. It explains fibre-filled engineering plastics, sealing faces, overmoulding, and how to match each part to a suitable machine.
Download PDFPDF · 207 KB
FAQs / Buyer Questions
Questions connector and cable assembly makers ask when they plan insert moulding for defence parts.
Which Injection Moulding Machine Is Used to Make Connector Backshells and Glands?
Parts with metal contacts or threaded shells are usually insert moulded on a vertical PVDL machine. Plain gland nuts and covers go to the E Series, and C Series machines take larger multi-cavity tools.Why Is a Vertical Machine Used for Insert Moulding?
On a vertical machine the lower mould half faces up, so contacts and threaded shells sit in their pockets by gravity while the mould closes. Loading is quicker and inserts are less likely to shift and be crushed by the clamp.When Are PPS or PEI Used Instead of Glass-Filled Nylon?
PPS and PEI are chosen where the part must survive solder reflow or meet a fire classification. They need higher barrel and mould temperatures, and PEI must be dried well, so heaters and dryer are sized to the grade.
How Is Flash Kept Out of the Contact Bores?
Insert pins and shut-off faces must fit closely, and every insert must sit correctly before clamping. Holding pressure is set high enough to fill thin walls but not so high that melt forces past the shut-offs into the bores.Can Pratishna Recommend a Machine for My Connector Backshell?
Yes. Share the part drawing, insert type and count, material grade, shot weight, mould dimensions, cavities and volume, and Pratishna Engineers will recommend a suitable machine.Does the Machine Suit Other Defence Electronics Parts Too?
Yes. Similar machines can mould gimbal housing parts, small rugged enclosure lids, battery pack housing parts and drone motor mounts, subject to the mould.
Technical Disclaimer
Disclaimer: The information provided in this webpage is for general informational and educational purposes only. It is based on technical references and industry information available at the time of preparation and may be subject to change. It does not constitute engineering, technical, commercial or professional advice, nor does it constitute a quotation, specification, warranty or contractual commitment by Pratishna Engineers.
Actual injection moulding machine and process requirements vary according to the component design, material, mould, production volume, machine configuration and operating conditions. The information, examples, calculations and recommendations provided should be independently evaluated and verified for the specific application before making any equipment, process or production decision. Information obtained from third-party sources remains subject to the accuracy and limitations of those sources.
Limitation of Liability: Pratishna Engineers makes no representation or warranty, express or implied, regarding the completeness, accuracy or suitability of the information for any particular application. To the extent permitted by applicable law, Pratishna Engineers shall not be liable for any loss, damage, cost or consequence arising from reliance on or use of the information contained in this webpage. Final machine selection, configuration and application suitability should be confirmed with Pratishna Engineers based on complete and accurate project requirements.
Talk to Our Engineers
Planning a New Injection Moulding Project?
Share your component, material, mould and production target. Our engineering team will help you identify the right machine configuration.
- Machine Sales
- +91 99690 38542
- Service Support
- +91 97689 28259
- Sales Email
- [email protected]